Best fit
Buyers building an initial budget before requesting a full quotation.
Price and quote factors
Bottle capping machine price depends on the closure, output speed, automation level, bottle handling and line scope. A simple semi-automatic tightening station is a different project from an automatic line with cap feeding and conveyors.
Search intent
This page is written for buyers comparing caps, bottle handling, cap feeding, torque or seal control and the wider machinery route before requesting a practical quotation.
Buyers building an initial budget before requesting a full quotation.
Prices without samples can be misleading because tooling, cap feeding and change parts can alter the project significantly.
Send the bottle/cap details, desired speed, automation level, number of formats and whether the project includes filling or labelling.
Related equipment
Most capping projects have more than one possible machine route. These related pages help narrow the specification before samples are reviewed.
Related equipment
Support for capper reliability, change parts, setup checks, training and spares planning.
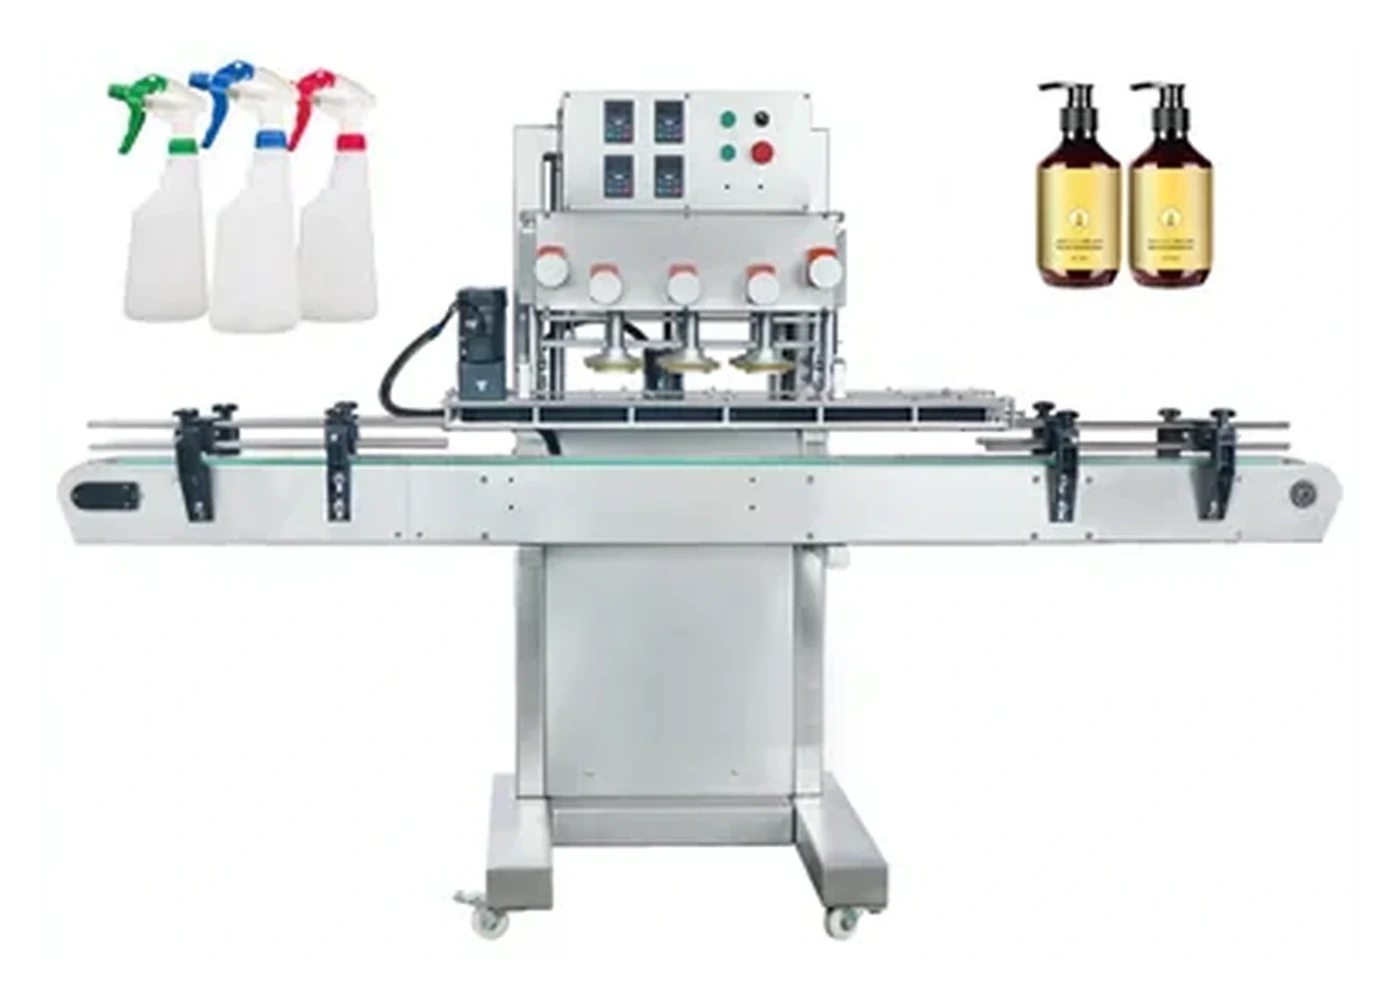
Catalogue photograph; the required configuration is confirmed during quotation.
View related page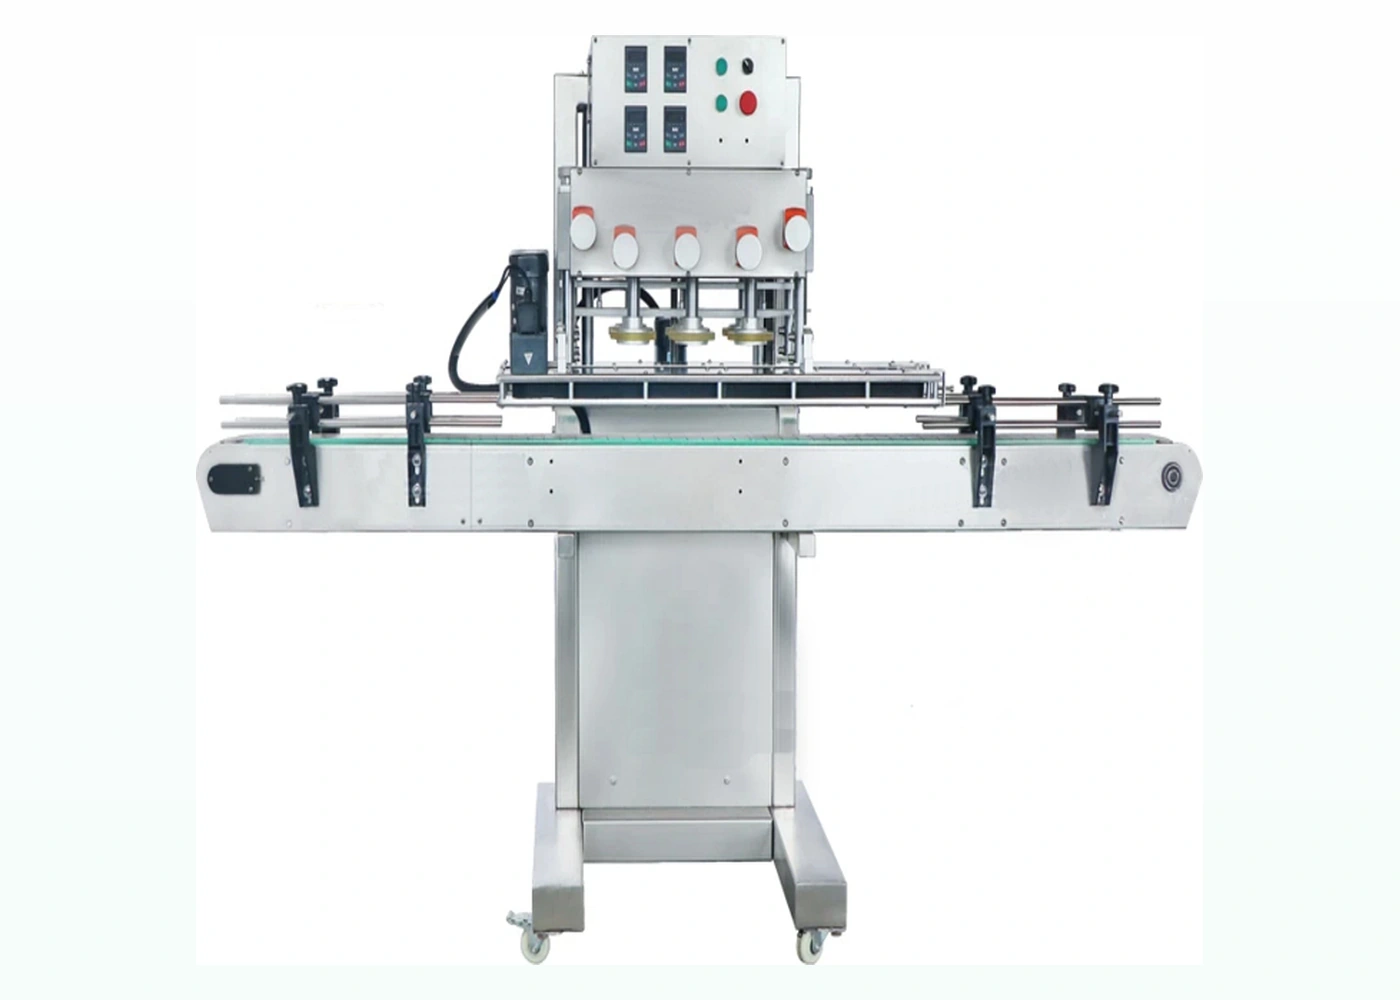
Related equipment
Guidance on torque, closure consistency and checks before a capping machine is specified.
Catalogue photograph; the required configuration is confirmed during quotation.
View related page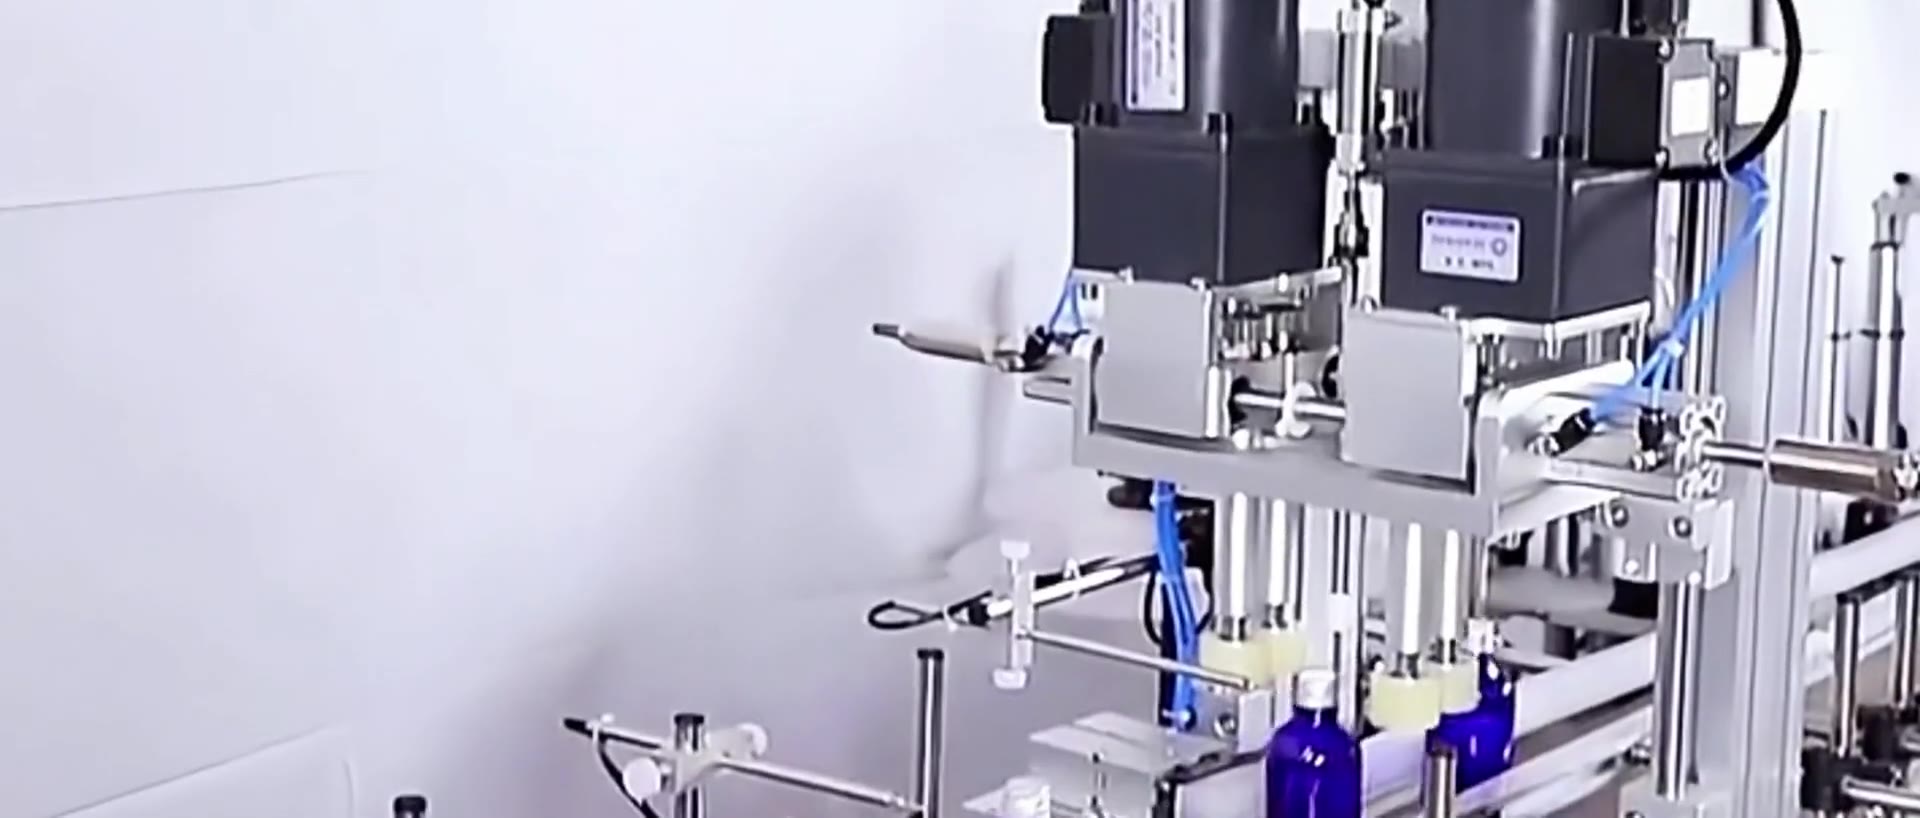
Related equipment
What to send when requesting a quotation for bottle cappers or complete bottle machinery.
Photograph of capping equipment on a bottle conveyor; the complete line scope is confirmed during quotation.
View related pageSpecification checklist
Clear information helps avoid the wrong capper, the wrong cap feeder or a line layout that cannot reach the intended output.
| Area | What to check |
|---|---|
| Bottle and cap samples | Confirm real production bottles, caps, neck finish, cap liner or band details and any variation between suppliers. |
| Output target | Confirm current and target bottles per minute, shift pattern, batch sizes and how often changeovers are expected. |
| Line integration | Check whether the capper is standalone or part of filling, conveying, labelling, coding and packing. |
| Operator method | Review cap placement, bottle loading, change parts, cleaning access, training and daily quality checks. |
Useful answers
These answers help production teams prepare a clearer enquiry before machine selection, sample testing or quotation.
Start with the closure and bottle. Check how the cap is applied, how the bottle is held, the target output and whether the line needs automatic or semi-automatic handling. Real samples are the best way to confirm suitability.
Send the bottle/cap details, desired speed, automation level, number of formats and whether the project includes filling or labelling.
Yes. The capping stage can be reviewed with filling, conveyors, labelling, coding, accumulation and operator access so the full line works as one production process.
Common causes include poor cap engagement, unstable bottles, unsuitable torque settings, caps that feed inconsistently, incorrect change parts, worn tooling or a mismatch between the capper and the closure style.
Send bottle photos, closure samples, target speed and line details so the right capping machine, cap feeder or complete bottle machinery route can be reviewed.
Capping decisions and practical evidence
A bottle capper price becomes useful when it names the closure method, format tooling, feeding arrangement and included site work. Keep optional work separate from the equipment needed to make the first approved format run.
Use three columns: included, optional and supplied by the customer. Apply them to the capper, feeder, conveyor, bottle supports, change parts, controls, installation, trials and documentation. An excluded feeder or transfer can materially change the usable system without changing the advertised capper price.
The site's documented Lancing models describe different application routes, not interchangeable packages. The bottle and closure, operator involvement and line interfaces determine the scope. A final figure should identify those assumptions, rather than presenting one machine price as the cost of every project.
Use the model library to choose which routes deserve review, then run the installed costs through the simple-payback calculator. The calculator uses your figures and does not create a Lancing quotation or infer a machine price.